


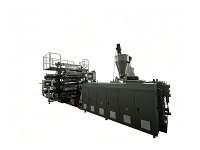


HDPE Gas Pipe Extrusion Line
This HDPE Gas Pipe Extrusion Line processes PE80 and PE100 grade high-density polyethylene into pressurized natural gas pipelines conforming to ISO 4437 and EN 1555 standards. Engineered for 24/7 continuous industrial operation, the line handles outer diameters from 16 mm to 630 mm across standard dimension ratios (SDR 9, SDR 11, SDR 13.6, SDR 17.6).
The system integrates a high L/D ratio single-screw extruder, a spiral distributor die head, multi-stage vacuum sizing and spray cooling, gravimetric dosing, continuous caterpillar haul-off, and planetary cutting. By maintaining precise thermal control and melt homogeneity, the equipment minimizes internal stress in the extruded pipe, ensuring long-term hydrostatic strength (MRS 10.0 MPa rating for PE100) and strict ovality control required for electrofusion and butt-fusion joining.
Production Process
Material Feeding & Dosing: PE100/PE80 virgin resin and yellow/black color masterbatch pass through a multi-component gravimetric dosing unit that adjusts screw speed and haul-off rate in real time to maintain pipe weight per meter within ±0.3%.
Plasticization & Extrusion: Material enters a grooved feed barrel where a specialized barrier screw melts resin under controlled shear temperatures (190°C–210°C) to prevent thermal degradation.
Co-Extrusion & Color Line Marking: Melt flows into a spiral distributor die head. A dedicated auxiliary single-screw extruder co-extrudes integrated yellow or orange identification stripes into the pipe's outer layer at the molecular level.
Vacuum Calibration: The extruded pipe blank enters a stainless-steel vacuum chamber (-0.03 to -0.06 MPa). Adjustable bronze calibration sleeves and water jets fix the outer diameter and initial wall geometry.
Multi-Stage Spray Cooling: Sequential immersion/spray cooling tanks lower core temperatures in gradients, eliminating thermal stress and preventing post-cooling wall deformation or sink marks.
Ultrasonic Inspection & Traction: An online 360° ultrasonic scanner calculates wall thickness and concentricity. The multi-caterpillar haul-off pulls the pipe at synchronized speed using vector frequency drives.
Planetary Cutting & Discharge: A chip-free planetary cutter performs square, chamfered cuts synchronized with line speed, discharging straight lengths to a tilting table or small-diameter pipes to a automatic dual-disc coiler.
Main Components
Main Extruder Unit:
• Screw & Barrel: 38CrMoAla alloy steel, ion-nitrided (depth 0.5–0.7 mm, surface hardness ≥950 HV) or optional bimetallic alloy coating for abrasive resistance.
• Screw Geometry: 33:1 or 38:1 L/D ratio barrier screw with mixing head for low-shear, uniform melt plasticization.
• Drive System: Siemens or SIMO AC motor coupled with a Sunlung/Transcyko high-torque gear reducer featuring an integrated heavy-duty thrust bearing.
Co-Extrusion Die Head:
• Body: 40Cr forged alloy steel with spiral flow channels, mirror-polished and hard-chrome plated internally.
• Striping Extruder: SJ-30/25 single-screw co-extruder for yellow/orange identification lines.
• Heating: Cast aluminum heating zones controlled via multi-channel PID loops.
Vacuum Calibration & Cooling Tanks:
• Material: Full Stainless Steel 304 construction.
• Vacuum System: Dual-chamber 6-meter vacuum tank with independent pressure controls and side-channel pumps.
• Cooling Circuit: 12-meter to 24-meter stainless spray tanks with stainless steel centrifugal pumps and quick-clean spray nozzles.
Haul-Off Unit:
• Configuration: 2-claw, 3-claw, 4-claw, 6-claw, or 8-claw caterpillar configurations based on pipe diameter.
• Control: Individual vector motors with encoder feedback synced via PLC to prevent slippage or pipe deformation.
Cutting & Stacking Equipment:
• Planetary Cutter: Hydraulic clamping, dust-free carbide saw blades, and integrated pipe end chamfering unit.
• Coiler (DN 16–63 mm): Torque-controlled dual-disc coiler with automatic traverse lay-flat winding.
Automation & Electrical System:
• PLC & HMI: Siemens S7-1200/1500 industrial controller with a 10-inch color touchscreen interface.
• Components: Schneider switchgear, ABB frequency inverters, RKC/Omron temperature modules.
Key Technical Advantages
Melt Homogeneity at Lower Processing Temperatures: The 38:1 L/D screw design incorporates barrier sections that melt PE100 resin at reduced thermal loads (190°C–210°C). This preserves polymer chain structures and guarantees compliance with ISO 4437 hydrostatic pressure tests (1000h at 80°C / 4.6 MPa).
Closed-Loop Wall Thickness Management: Combining gravimetric feeding with an online ultrasonic scanner keeps wall thickness variance within Δt≤±0.1 mm. Over-gauging is eliminated, reducing raw material usage by 2.5% to 4.0% per shift.
Strict Ovality & Roundness Retention: Multi-stage vacuum regulation (-0.03 to -0.06 MPa) combined with multi-point cooling spray geometries holds pipe ovality within ≤1.2%, ensuring immediate fit-up for field welding.
Technical Specifications
|
Model |
Pipe Range (OD) |
Extruder Model |
Output Capacity |
Installed Power |
Line Dimensions (L × W × H) |
|
PE-GAS-63 |
16 mm – 63 mm |
SJ-65/33 |
180 – 220 kg/h |
110 kW |
32 m × 2.5 m × 2.8 m |
|
PE-GAS-110 |
32 mm – 110 mm |
SJ-75/38 |
280 – 350 kg/h |
145 kW |
38 m × 2.8 m × 3.0 m |
|
PE-GAS-250 |
75 mm – 250 mm |
SJ-90/38 |
450 – 550 kg/h |
220 kW |
48 m × 3.2 m × 3.2 m |
|
PE-GAS-400 |
110 mm – 400 mm |
SJ-120/38 |
650 – 750 kg/h |
310 kW |
56 m × 3.5 m × 3.5 m |
|
PE-GAS-630 |
315 mm – 630 mm |
SJ-150/38 |
800 – 950 kg/h |
420 kW |
65 m × 4.0 m × 3.8 m |
Typical Applications
Pipes manufactured on this equipment meet standard specifications for underground pressurized gas networks:
Natural Gas Mains & Feeder Lines: SDR 11 / SDR 9 pipes operating under pressures up to 10 bar.
LPG & Town Gas Distribution: Residential and industrial fuel gas piping systems.
Biogas Conveyance Systems: Gas transfer lines in agricultural and industrial biogas processing plants.
Compliance Standards: ISO 4437-2, EN 1555-2, ASTM D2513, AS/NZS 4130.
How to Select the Right Machine
Use the breakdown below to match line sizing with target production requirements:
|
Target Pipe Range |
Primary Wall Ratings |
Target Output |
Recommended Line Model |
Downstream Setup |
|
DN 16 – 63 mm |
SDR 9, SDR 11 |
150 – 200 kg/h |
PE-GAS-63 |
Auto Dual Coiler |
|
DN 32 – 110 mm |
SDR 11, SDR 17.6 |
250 – 320 kg/h |
PE-GAS-110 |
Coiler & Planetary Cutter |
|
DN 75 – 250 mm |
SDR 11, SDR 13.6, SDR 17.6 |
400 – 500 kg/h |
PE-GAS-250 |
Planetary Cutter & Stacker |
|
DN 110 – 400 mm |
SDR 11, SDR 17.6 |
600 – 700 kg/h |
PE-GAS-400 |
Planetary Cutter & Stacker |
|
DN 315 – 630 mm |
SDR 11, SDR 17.6, SDR 21 |
800 – 900 kg/h |
PE-GAS-630 |
Heavy Duty Planetary Cutter |
Quality Control & Factory Testing
Every line undergoes a two-stage inspection process prior to factory acceptance and packing:
Stage 1: Static Assembly & Electrical Audit
Mechanical alignment checks via precision laser leveling across frame bed tracks.
Dynamic balancing verification of drive shafts, gearbox input/output couplers, and cutter heads.
Electrical safety test verifying insulation resistance (>10 MΩ) and grounding continuity.
Stage 2: 8–12 Hour Continuous Factory Acceptance Test (FAT)
Equipment runs on PE100 raw material at maximum operating speed. Acceptable operating parameters must meet the following metrics before customer sign-off:
• Melt Pressure Stability: Pressure fluctuation at the die head kept within ±0.8 MPa.
• Thermal Drift: Barrel temperature variations maintained within ±1.0∘C across all zones.
• Weight Accuracy: Extrusion weight variation across 6 timed pipe samples held within ≤±1.5%.
• Vibration Limits: Gearbox bearing housing vibration velocity remains below 2.5 mm/s.
Why Work with Us
In-House Precision Machining: Components such as barrels, dies, and frames are processed using CNC machine tools, laser cutting centers, and dynamic balancing equipment to maintain strict tolerance control.
Standardized Spare Part Availability: Critical wearing parts (heater bands, thermocouples, pressure transducers, seals, and cutter blades) are maintained in stock to support dispatch within 60 days for standard orders.
Engineering Field Support: Technical assistance includes layout engineering, power line planning, overseas installation supervision, material formulation adjustment, and machine operator training.
FAQ
Hot Tags: hdpe gas pipe extrusion line, China hdpe gas pipe extrusion line manufacturers, suppliers, factory, PE Pipe Extrusion Line, PE Pipe Producing Line, PE Pipe Production Line, Pipe Extrusion Line, PP Pipe Extrusion Line, PVC Pipe Producing Line
You Might Also Like


Send Inquiry