


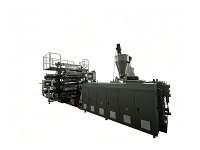


UPVC Pipe Extrusion Line
This modular UPVC Pipe Extrusion Line converts dry-blend PVC powder or CPVC compound into rigid pressure and non-pressure piping from 16 mm to 630 mm outer diameter (OD). Powered by conical twin-screw extruders (SJZ series), the line produces pipes fully compliant with ISO 1452, ASTM D1785, DIN 8061/8062, and BS EN 1401 international standards.
To maximize plant throughput across varying dimensional bands, the system supports multi-strand and single-strand extrusion modes: 4-outlet configuration for small electrical conduits (DN16–32), double-outlet for mid-range piping (DN16–110), and single-outlet for heavy-duty water and municipal sewer lines (DN50–630).
Production Process
Material flows sequentially through ten synchronized engineering stages:
Dosing & Feeding: UPVC resin powder, thermal stabilizers (Ca-Zn/Lead/Tin), impact modifiers, and CaCO₃ filler enter the feed throat via an automatic spring loader or vacuum conveyor equipped with continuous level sensors.
Plasticization & Extrusion: Counter-rotating conical twin screws subject the compound to controlled mechanical shear and gradient thermal zones, melting the polymer without thermal degradation or chain scission.
Vacuum Melt Degassing: A liquid-ring vacuum pump vents trapped air, moisture, and volatile gases at -0.095 MPa, preventing micro-porosity and wall void defects.
Die Head Flow Distribution: Melt flows into a 40Cr forged spider die head or spiral distributor die, maintaining uniform velocity and wall concentricity across all stream outlets.
Vacuum Calibration & Primary Cooling: The molten tube enters a stainless-steel vacuum calibration tank. A high-precision bronze or stainless calibration sleeve establishing exact outer diameter (OD) under negative pressure, while continuous chilled water spray solidifies the outer shell.
Multi-Stage Water Cooling: Secondary spray cooling tanks lower the core temperature below the glass transition threshold (Tg), relieving internal thermal stresses.
Synchronized Caterpillar Haul-Off: Multi-claw caterpillar pullers (2 to 8 claws depending on pipe OD) supply stable linear pulling tension. Speed regulation is continuously synchronized with the extruder via digital encoder feedback.
Chipless / Orbital Cutting: Automatic planetary saws or chipless rotary knives execute burr-free perpendicular cuts according to programmed pipe lengths. Integrated vacuum extraction removes residual swarf.
Inline Belling / Socketing (Optional downstream): Pipe ends are automatically heated and molded with socketing units to form solvent-cement sockets or rubber-ring (R-R) elastomeric joints.
Pneumatic Discharge Stacker: Finished pipe segments drop onto a pneumatic tilting table for final dimensional audit, quality sampling, and packaging.
Main Components & Technical Standards
Critical mechanical, drive, and control sub-assemblies are built with standardized tier-1 industrial components to ensure global spare parts availability and interchangeability:
|
Sub-Assembly |
Standard Component Brand / Spec |
Engineering Function & Technical Specification |
|
Main Motor |
Siemens / SIMO AC Motor |
Variable frequency drive (VFD) regulated motor providing constant output torque across low and high RPM ranges. |
|
Extruder Gearbox |
Taiwan Sunlung / JC Brand High-Torque Gearbox |
Heavy-duty helical reducer with integrated high-capacity thrust bearing block absorbing axial backpressures ≥ 35 MPa. |
|
Screw & Barrel |
38CrMoAla Alloy Steel (Nitride depth: 0.5–0.7 mm; Hardness: ≥ 950 HV) / Optional Bimetallic Layer |
Conical twin-screw geometry optimized for PVC shear sensitivity; features closed-loop internal oil cooling for active screw core temperature control. |
|
Extrusion Die Head |
40Cr Forged Alloy Steel with Mirror-Polished Hard Chrome Plating |
Spider or spiral manifold design for uniform flow distribution; equipped with multi-zone cast-aluminum ceramic heaters. |
|
Main Inverter & VFD |
Fuji / ABB Frequency Inverters |
Closed-loop speed control for main drive, feeder, haul-off, and cutting unit. |
|
PLC Control System |
Siemens PLC (S7-1200 / S7-1500) & Touchscreen HMI |
Centralized operational control with recipe storage, real-time temperature tracking, fault diagnostics, and Industrial Ethernet / Modbus interface. |
|
Temperature Control |
Japan RKC PID Controllers / Integrated Siemens Modules |
Solid-state relay (SSR) control maintaining barrel thermal stability within ± 1°C. |
|
Low-Voltage Electrics |
Schneider Electric / ABB |
IP54-rated control enclosure housing circuit breakers, contactors, and thermal overload interlocks. |
|
Pumps & Hydraulics |
Stainless Steel Impeller Pumps / Italy Oiltec Valves |
Liquid-ring vacuum pumps, high-head water pumps, and hydraulic valve blocks for stable mechanical clamping and movement. |
Key Advantages
Formulation Flexibility for High CaCO₃ Loading: Deep-nitrided conical twin screws provide uniform mixing at lower shear temperatures, allowing processing of formulations containing up to 30–50 phr Calcium Carbonate without screw scuffing or melt degradation.
Heavy-Duty Frame Rigidity: Structural machine frames are welded from thick-walled steel tubing and stress-relieved prior to multi-axis CNC machining, preventing frame misalignments during long-term continuous operation.
Optimized Energy Efficiency: Insulated ceramic barrel heaters with forced-air cooling shrouds and closed-loop oil temperature regulation minimize power consumption (0.22–0.28 kWh/kg).
Closed-Loop Speed Matching: Digital encoder feedback between the extruder main motor, feeder, and caterpillar haul-off maintains uniform wall thickness during line startup and speed transitions.
Clean Chipless Cutting: Planetary cutting units feature orbital blades and integrated dust extraction, producing square, smooth pipe ends ready for immediate socketing.
Technical Specifications Matrix
|
Model Code |
Pipe Diameter Range (OD) |
Extruder Model |
Die Outlets |
Max Output (kg/h) |
Installed Power (kW) |
Line Length (m) |
|
GF-32-4 |
Ø16 mm – Ø32 mm |
SJZ-65/132 |
4-Outlet |
200–250 |
101 |
18 |
|
GF63-2 |
Ø16 mm – Ø63 mm |
SJZ-65/132 |
2-Outlet |
250–300 |
105 |
23 |
|
GF110-2 |
Ø50 mm – Ø110 mm |
SJZ-80/156 |
2-Outlet |
350–450 |
140 |
27 |
|
GF160 |
Ø50 mm – Ø160 mm |
SJZ-65/132 |
1-Outlet |
200–300 |
115 |
26.5 |
|
GF250 |
Ø90 mm – Ø250 mm |
SJZ-80/156 |
1-Outlet |
300–400 |
145 |
28 |
|
GF400 |
Ø200 mm – Ø400 mm |
SJZ-80/156 |
1-Outlet |
300–400 |
210 |
30 |
|
GF630 |
Ø315 mm – Ø630 mm |
SJZ-92/188 |
1-Outlet |
600–700 |
340 |
41 |
Typical Applications
Electrical Conduit Piping: Small-diameter UPVC conduit (Ø16 mm–Ø32 mm, 4-outlet output) for cable protection and building electrical wiring.
Potable Water Supply Lines: Medium-diameter UPVC pressure pipes (Ø20 mm–Ø160 mm, PN6 to PN25 ratings) complying with ISO 1452 and DIN 8062 standards.
Agricultural Irrigation Networks: Medium piping for sprinkler mainline distribution, borehole casings, and agricultural drainage networks.
Building Sanitary & Sewerage: Soil, waste, and vent (SWV) pipes (Ø50 mm–Ø200 mm) and underground gravity sewer lines complying with BS EN 1401 standards.
Industrial Chemical Piping: Chemical-resistant UPVC and CPVC piping (up to Ø630 mm) for industrial fluid transport and storm-water drainage trunks.
How to Select the Right Machine Configuration
|
Selection Criteria |
Engineering Consideration |
Recommended Line Configuration |
|
Target Outer Diameter (OD) |
Conduit production vs large municipal drainage pipe. |
Ø16–32 mm: Choose GF-32-4 (4-Outlet) |
|
Hourly Output (kg/h) |
Target annual tonnage of processed PVC powder. |
Up to 300 kg/h: SJZ-65/132 Extruder |
|
Material Formulation |
Resin K-value (K-67 vs K-57), CaCO₃ phr ratio, and stabilizer type. |
Formulations exceeding 30 phr CaCO₃ require tungsten-carbide bimetallic screws/barrels to mitigate abrasive mechanical wear. |
|
Pipe Jointing Requirement |
Plain square ends, solvent socket, or rubber-ring (R-R) joint. |
Integrate an online automatic belling machine directly downstream from the cutting station. |
Quality Control & Factory Acceptance Testing (FAT)
Factory Quality Verification & Test Protocols
In-House Machining & Component Audits:
Raw steel (38CrMoAla, 40Cr) spectro-analysis and metallurgical certificates.
Dynamic balance testing for screws and high-speed cutting assemblies.
Alignment verification for gearbox output shafts and vacuum sealing tanks.
Factory Acceptance Test (FAT):
72-Hour Continuous Load Run: Full machine trial using standard UPVC compound or buyer-supplied powder.
Dimensional & Wall Audits: Laser outer diameter and wall thickness roundness verification across produced samples.
Thermal & Electrical Audit: Infrared thermal inspection of heat zones; power consumption monitoring under full output load.
Why Work with Us
15+ Years Machine Building Knowledge: Specialized engineering teams experienced in international plant layouts, screw design optimization, and formulation troubleshooting.
Global Spare Parts Availability: Core operational spares (barrel heaters, thermocouples, pressure sensors, seals, and cutter blades) maintained in inventory for rapid dispatch. Standard machine lead time within 60 days.
Field Service & Commissioning Support: Overseas technical assistance available across South Asia, the Middle East, Africa, and Europe for installation, startup, and operator training.
Complete Engineering Documentation: Machine shipments include complete electrical schematics, mechanical drawings, spare parts catalogs, and step-by-step operating manuals in English.
FAQ
Hot Tags: upvc pipe extrusion line, China upvc pipe extrusion line manufacturers, suppliers, factory, PE Pipe Extrusion Line, PE Pipe Producing Line, PE Pipe Production Line, Pipe Extrusion Line, PP Pipe Extrusion Line, PVC Pipe Producing Line
You Might Also Like


Send Inquiry