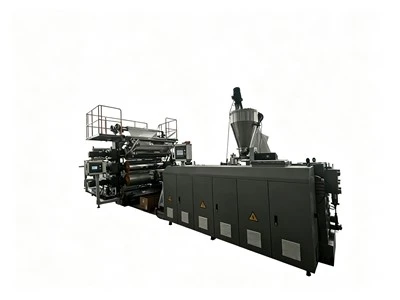
If you're running a WPC door extrusion operation or even just looking to level up your machine game, precision is everything. Let's be real-nothing kills a production day faster than inconsistent door thickness, warped edges, or spots where the wood-plastic composite doesn't bind right. As the team behind a WPC Door Extruder supplier, I've seen so many players skip small, fixable steps that lead to big, avoidable waste. Today, I'm breaking down the realistic, science-backed tweaks we've tested over years of supporting extrusion lines (not just for doors, but also stuff like the PVC Wall Panel Production Line and PVC Flooring Extrusion Line our clients love). No jargon, no fluff-just what actually works.
First off, let's start with the basics people tend to overlook: raw material prep. I know, I know, it sounds boring, but WPC is a mix of wood flour, plastic resin, stabilizers, and sometimes colorants. If those components aren't measured or blended right, even the fanciest extruder will spit out junk. We once had a client bring us parts that were 10% too thin across 30-foot runs, and when we checked, they were just scooping wood flour by hand instead of using an automated batch weigher. Hand scooping leads to 2-3% variability in wood content, which directly changes melt viscosity-thicker when there's too much wood, thinner when too little.
Another raw material mistake: moisture control. Wood flour absorbs water like a sponge, and if you don't dry it out completely before extrusion, that water turns to steam when hit with heat. The steam creates bubbles in the WPC, which mess up the dimensional precision of the finished door. We always recommend drying wood flour to under 0.5% moisture content, and using a moisture analyzer to spot-check every batch. That little step cut one of our repeat clients' bubble defects by 82% in a month-worth the $200 dryer investment, easy. Also, make sure you're using high-quality WPC resin; cutting corners on cheap recycled resin might save a buck short-term, but it leads to inconsistent melting, so that's a no-go if you care about precision.
Next up, the extruder itself-wait, no, not just any extruder, the WPC Door Extruder you're running. A lot of operators don't realize that the extruder's screw and barrel setup is tailored for WPC, not PVC. If you're using a general-purpose PVC screw (even if you used it for the PVC Door Extruder line last quarter), it's not going to mix the wood and plastic evenly. WPC needs a screw with a deeper feeding section to handle the bulky wood flour, and a gradual compression ratio (around 1.5:1 to 2:1) to avoid shearing the wood fibers too much. Sheared fibers make the WPC less structurally consistent, which leads to warping when the door cools. We've had clients switch to WPC-specific screws and see thickness variability drop from ±0.8mm to ±0.2mm-game changer.
Then there's the barrel temperature profiling, which is way more important for WPC than people think. Too hot, and the plastic degrades, leaving discolored spots and weak areas. Too cold, and the mix doesn't melt evenly, leading to lumps that mess up the die opening. The sweet spot we've landed on with our machines is: feeding zone at 140-150°C, transition zone at 160-175°C, metering zone at 180-190°C. Don't just set it and forget it-use infrared thermometers to track barrel temp every hour, and adjust if you see the melt consistency change. Pro tip: if you're moving from a smaller batch to a larger one, wait 20 minutes for the barrel to stabilize; sudden temp shifts throw off precision big time.
Now, the die and calibration section-this is where precision gets final, not just in the mix. The die is the part that shapes the WPC into the door profile, and even a tiny imperfection there ruins the whole run. First, make sure the die is aligned properly. I've seen operators tighten one bolt too much and warp the die plate, so the opening wasn't uniform across the width. That leads to some spots coming out thicker than others, which means the door won't fit into its frame. We recommend using a dial indicator to check die flatness every 500 hours of operation-fixing a warped die takes 20 minutes and stops hours of scrap.
Calibration is the next step, and it's where a lot of people skip calibration vacuum settings. The vacuum calibration table pulls the extruded WPC against a cooled metal profile, locking in the dimensions while it's still malleable. If the vacuum is too high, it will pull the WPC inward, making the door narrower; too low, and it won't hold the shape, leading to bulges. We test our WPC Door Extruders at our facility with a 12-inch door profile, and the sweet spot is usually 8-12 inches of mercury for vacuum, depending on the WPC mix. Also, make sure the calibration table's cooling water is at the right temp-10-15°C is ideal. If the water is too warm, the WPC cools unevenly, causing residual stress that leads to warping later. We once had a client with a warping problem that turned out to be a 2°C higher cooling water temp-fixed that and warping dropped by 70%.


Then there's the haul-off unit, which pulls the door at a consistent speed through the calibration and cooling line. Speed variability is a huge culprit for poor precision. If the haul-off speeds up for 10 seconds, the door gets thinner; if it slows down, it gets thicker. We use a laser speed sensor (way better than wheel encoders, which slip on smooth WPC) to track haul-off speed every 5 seconds. For WPC door extrusion, the speed should be around 2-4 meters per minute, depending on the profile thickness-thicker doors need slower speeds. Also, make sure the haul-off rollers are clean and aligned; a piece of debris between the rollers will make a dent, and misaligned rollers will bend the door slightly, throwing off measurements.
Wait, let's talk about maintenance, because this is the long-game for precision. Extrusion machines are like cars-if you skip oil changes and tune-ups, they break down or get sloppy. For WPC machines, we recommend daily checks: clean the screen changer (old screens get clogged, leading to uneven pressure), check the screw for wear (a worn screw has less output pressure, leading to inconsistent melt), and inspect the die for buildup (WPC residue hardens over time and builds up on the die lips, leading to uneven surfaces). Every month, do a full check of all motors, rollers, and sensors-even small issues like a loose sensor wire can cause speed or temp fluctuations that add up to big precision problems.
Also, operator training-this is the thing most companies overlook. A new operator who's only used a PVC extrusion line (maybe the PVC Flooring Extrusion Line or PVC Wall Panel Production Line) won't know that WPC reacts differently to heat and speed. For example, when purging the extruder, WPC needs a different purge compound than PVC-using PVC purge on WPC can leave residue that messes up the next run's precision. We offer hands-on training for all our WPC Door Extruder clients, because we've seen so many mistakes come from operators not knowing the specific needs of WPC vs. other materials. Even a 2-hour refresh course for seasoned operators can cut defect rates by 30% alone.
Let's bust a common myth here: more expensive parts don't always equal more precision. Sure, high-end sensors are good, but a lot of the time, it's the small, consistent tweaks that make the difference. For example, we had a client who spent $10k on a new high-tech sensor, but didn't realize their haul-off rollers were misaligned. Fixing the rollers (free, just labor) and calibrating the speed (1 hour) gave them better precision than the sensor did. It's about balancing machine hardware with process steps, not just buying the latest gear.
Another thing: material testing between runs. If you change wood flour suppliers, or switch resin types, do a small test run first. Extrude a 1-meter section, measure its thickness across the entire length, check for bubbles, and adjust temp, speed, or vacuum before running a full order. We always tell our clients not to jump straight into a big production run after a material change-test first to avoid tons of scrap.
Now, let's wrap this up with a quick recap for anyone scanning: get your raw materials right (measure, dry, pick good components), use a WPC-specific screw and barrel temp profile, keep your die aligned and calibration vacuum/cooling in check, make sure haul-off speed is consistent, do regular maintenance, and train your operators. All of these steps tie into the equipment we supply-our WPC Door Extruder is built with these exact profiles and easy maintenance points, but even if you're using another brand, these tips apply.
If you're looking to upgrade your line, or just troubleshoot those stubborn precision issues, feel free to reach out. We've supported clients with everything from small, single-door lines to large-scale production facilities, and we know how to get those door dimensions spot-on. Whether you're dealing with warping, thickness variability, or just inconsistent output, we can help you work through it.